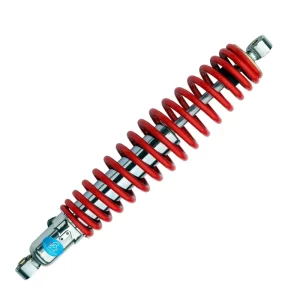
An off road coilover shock can lose its body before the valving wears out. The first failure I look for is not seepage at the seal, but a coating that has cracked, lifted, or worn through on the outer tube. For off road coilover shocks, surface coating options determine how fast abrasive mud, stone hits, and road film turn a fresh body into a corrosion point. The finish should be specified as a functional surface, not selected by color. That distinction is the difference between a housing that survives several seasons and one that starts rusting in the first wash bay.
How Does the Finish on Off Road Coilover Shocks Fail First?
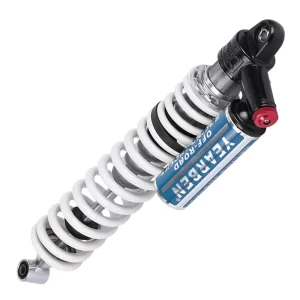
For a coilover, the body carries both internal pressure and the spring load. The coating on the outer tube has two jobs: corrosion protection and impact resistance. Most field failures start at edges: the lower spring seat thread, the spring preload ring contact line, and the reservoir bracket weld zones. I have seen bodies returned where the main tube was clean, but the coating under the spring preload collar had cracked from repeated clamping and let moisture sit against raw steel.
The failure sequence is usually the same: a coating microcrack forms, water and chlorides collect at the edge, the steel body oxidizes under the film, and the finish lifts in sheets. Once the film lifts, the piston rod seal may still hold, but the body becomes an eyesore and then a structural concern at the hard points.
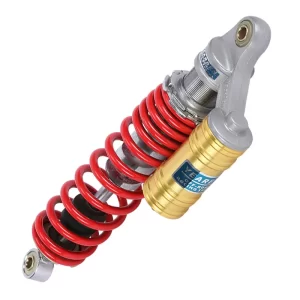
Which Surface Coatings Are Used on Off Road Coilover Shocks?
Not every coating works across the entire shock. The piston rod needs a hard chrome or ceramic-reinforced chrome surface because it slides under pressure and must hold oil. The outer tube has different requirements: it sees corrosion, mechanical contact, and heat. The most common factory finishes I specify are zinc-nickel plating, electroless nickel, powder coat, anodizing on aluminum bodies, and black oxide for budget or indoor-only applications.
The choice starts with base material, not color. A steel body cannot be anodized. An aluminum body cannot be zinc plated. That alone eliminates half the catalog options when a customer is trying to match an existing vehicle.
| Coating | Base material | Main advantage | Common off-road failure mode |
|---|---|---|---|
| Zinc-nickel plating | Steel body | Sacrificial corrosion resistance with controlled thickness | Thin coverage at thread crests and bracket edges |
| Electroless nickel | Steel or aluminum | Uniform deposit on complex bores and threads | Harder to touch up after field damage |
| Hard chrome | Piston rod | Sealing surface and wear life | Not a body finish; pitting develops if the film breaks |
| Anodizing | Aluminum reservoir or body | Light weight and controlled surface | Edge wear from clamps and spring seats |
| Powder coat or epoxy | Steel body or reservoir | Thick impact layer | Chips at sharp edges and can mask pre-coat steel defects |
Why Does the Piston Rod Still Use Hard Chrome?
The rod’s surface finish is not cosmetic. The seal lip has to shear the oil film cleanly at high velocity. A hard chrome surface holds the right surface energy and wear resistance. On off-road coilover shocks, the rod also sees mud abrasion on the exposed section. We keep hard chrome as the default rod coating because any substitute has to prove it does not shorten seal life during extended dust cycle testing.
When Does an Anodized Aluminum Body Make Sense?
Anodized aluminum appears on piggyback reservoirs and some lightweight coilover bodies. It makes sense when the complete assembly is weight sensitive, such as a sand rail or a race buggy. The limitation is mechanical. Anodized edges mark easily under spring clamps and aluminum threads gall when the preload ring is adjusted. We treat anodize as an acceptable exterior surface only when the customer understands the maintenance tradeoff.
How Do You Match a Coating to Your Operating Conditions?
Most of the answer is not in the coating data sheet. It is in how the shock is cleaned and stored. A desert racer needs impact resistance because sand removes a finish by erosion. A muddy trail rider needs crevice protection because wet soil stays packed around the spring seat for days. A coastal fleet truck needs sacrificial protection with an active corrosion cell because salt spray reaches areas a film cannot seal.
For general off-road use, I start with a zinc-nickel plated steel body or an electroless nickel finish. Both are thin enough to preserve thread dimensions and strong enough to survive bracket installation. For a vehicle that pressure washes after every run, I take a different route. Pressure washers drive water into the spring preload ring and reservoir bracket gaps. No coating alone solves that; the specification must include edge rounding and sealed fasteners, not just a thicker film.
If your program involves saltwater exposure, regular salt-brine road film, or coastal sand, coating choice needs to be confirmed with an actual corroded part sample or a salt-spray test panel before you finalize the bill of materials. Send your operating environment and body finish requirement to info@yearbenshocks.com and we will match the coating to the failure mode.
What Should You Demand from a Coilover Shock Coating Supplier?
A coating is not a single number. The same zinc-nickel specification can be plated at 8 microns or at 14 microns, with different edge coverage and completely different thread behavior. I ask for three things before releasing a purchase order: the plating thickness range, the adhesion method, and the neutral salt-spray pass criteria with a stated failure definition.
The most common gap is not adhesion. It is that the plater measures thickness on a flat coupon, while the shock body carries threads, weld zones, and sharp bracket edges. Those are exactly where corrosion starts. When I audit a coating source for coilover shock bodies, I look at masked threads and sharp-edge coverage before I look at a polished display part.
A second check is whether the coating supplier understands the assembly process. If a weld point is painted over with a fill layer, the coating can pass visual inspection and fail in service. If a body is powder coated before the reservoir mount is welded, the coating around the heat-affected zone burns off. That leaves an uncoated ring exactly where water collects. The process route has to be ordered the same way every time, and that belongs in the supplier quality plan, not in the marketing description.
Which Coating Specification Details Should You Send to a Factory?
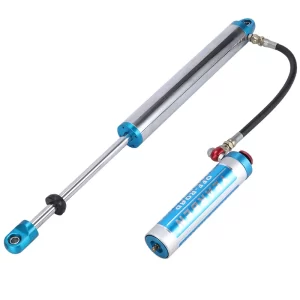
Matching a surface finish without a physical sample is guesswork. Buyers who send only a photo of an old shock body often receive a quote that changes after plating because the thread class, bore tolerance, and bracket weld condition are not on the print. We prefer to quote a finished coilover shock coating against five pieces of information: the body material, the required thread form, the operating environment, the pressure wash or storage method, and a failed sample if one exists.
If you are building an ATV, UTV, buggy, or 4×4 platform and need off-road coilover shock bodies with a coating that will hold through mud, salt, or sand, send the part number and the failure mode to info@yearbenshocks.com or call +86-523-86566899. We will confirm the coating stack, edge treatment, and sample lead time before you freeze the specification.
What Else Should Engineers Ask About Shock Body Coatings?
What is the difference between hard chrome and decorative chrome on a coilover?
The difference is pore structure and thickness. Hard chrome on a piston rod is a thick, wear-resistant deposit built to carry the seal lip and survive shaft movement. Decorative chrome on a body or exposed part is a thinner bright layer that looks good until the first stone chip exposes base metal. Off-road coilover shocks need hard chrome only where the seal rides. Using decorative chrome on loaded surfaces is a visual choice, not a durability choice. If the rod is pitted, chrome cannot fix the base steel.
Is anodizing enough for a coilover shock body?
Anodizing is often treated as a complete corrosion solution, but on a threaded coilover body it is weaker at the edges where the spring seat clamps. The coating protects the aluminum surface, yet a sharp edge or a worn thread can expose bare alloy and start galvanic attack, especially if a steel preload ring is fitted. We use anodizing on reservoirs and lightweight assemblies more than on high-load coilover bodies. If the body carries structural threads and is adjusted in service, a plated steel or a hard anodized and sealed aluminum body is the safer route.
Does powder coat trap corrosion under the film?
It depends on the pre-coat condition and the edge profile. If the steel is prepared and sealed before coating, powder coat holds up better than liquid paint. But if a small cut or clamp scrape lets water under the film, powder coat can hide rust until a bubble appears. The corrosion does not come from the powder itself. It comes from the body surface not being clean, dry, and free of light rust before coating. For coilover shocks, I prefer zinc-nickel under a thin epoxy layer rather than a heavy powder layer over bare steel.
Which coating should a buyer choose for a saltwater vehicle?
In off-road coilover shock programs I have worked on, saltwater survival usually comes down to two conditions: whether the vehicle is rinsed after use and whether the body has exposed edges near the spring collars. If it is rinsed and stored dry, zinc-nickel with sealed edges is a workable balance. If it runs on a beach and is parked without washing, no single coating will hold up for long; the body also needs a maintenance schedule and close inspection of the lower spring seat. Share your operating environment and we will confirm the coating stack and salt-spray criteria that fit your program.
If you’re interested, check out these related articles:
Twin-Tube-Hydraulic-Seat-Damper-28MM
Best-Shocks-And-Springs-For-Trucks
Hydraulic-Seat-Damper-Cylinder-Diameter-24MM