Most bypass shock inconsistency between runs gets blamed on valving before the real cause is measured. I have spent twenty years debugging this problem on ATV, UTV, and desert race applications. Two shocks built from the same drawing can arrive at the dyno with a measurable force spread, and the gap is rarely one clean adjustment. Nitrogen charge, oil fill volume, shim stack orientation, needle bleed, and rod seal friction stack up in ways that look like tuning error. The correction starts with documenting the full run setup, not swapping clickers.
What Does Bypass Shock Inconsistency Look Like on a Dyno?
Run-to-run bypass shock inconsistency rarely appears as a simple high force or low force. It shows up as a curve that crosses the good run at one shaft speed and separates at another. A bypass shock has fixed internal bleed plus external tubes that open at different points in the stroke. When nitrogen pressure or oil fill differs, the low-speed portion moves first. When a shim stack is wrong, the knee in the curve moves later. The most useful first step is to run the same unit three times and record rod temperature, charge pressure, and force at three shaft speeds before opening anything.
Which Build Variables Cause Bypass Shock Inconsistency Between Runs?
Most assembly errors are invisible from the outside. A shim stack can be assembled with one shim reversed, one missing, or one thickness substituted for another. Piston nut torque changes stack preload, which shifts the point where the stack opens. A bleed screw set half a turn different from the drawing changes low-speed force before the bypass tubes even begin working. Check valve orientation in the bypass tube controls whether the shock sees compression, rebound, or both during that section of travel. We have pulled apart pairs where one side had the rebound stack one shim off, and the dyno difference disappeared once the stacks matched.
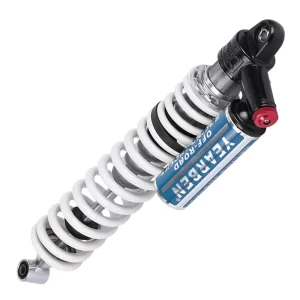
Nitrogen charge and oil fill matter just as much as the shim stack. A shock charged before cycling shows a different stabilized pressure than one charged after cycling. Oil fill height controls the gas pocket size and the piston movement point. Too little oil produces a dead spot at the start of the stroke, while too much oil can spike at full compression. Both errors show up as run-to-run inconsistency before they are visible as leakage.
| Variable | What changes between runs | Correction |
|---|---|---|
| Nitrogen charge | Force offset and cavitation point shift | Cycle, bleed, and recharge to the same logged pressure |
| Oil fill volume | Gas pocket size changes low-speed build feel | Fill by height after vacuum bleed, then verify after cycling |
| Shim stack | Stack preload or thickness changes knee force | Lay out both stacks side by side against the drawing |
| Bleed screw | Low-speed force changes with a partial turn | Lock setting and record turns from seated |
| Rod seal friction | Hysteresis changes before the valve opens | Warm up both shocks and compare seal drag |
If your program involves nitrogen fade or oil fill variation that is difficult to measure outside a factory, confirm the charge and fill procedure before your next valving change. Send the two mismatched dyno sheets and charge logs to info@yearbenshocks.com. We will map the spread to a build variable.
How Do You Fix Bypass Shock Inconsistency Without Guessing?
Start with the shock that runs correctly, not the one that feels wrong.
- Warm up both shocks on the same dyno until rod temperature stabilizes.
- Record force at three piston speeds and note where the curves separate.
- Log nitrogen pressure, oil height, bleed screw turns, and piston nut torque.
- Disassemble both units and lay out every shim in order against the drawing.
- Reassemble with the same oil batch, same fill height, same charge pressure, and the same torque.
- Cycle each shock five times, then run the dyno test again. If the spread remains, inspect the piston band and rod seal for drag.
Do not tune one shock to compensate for an assembly difference in the other. That masks the problem and produces a pair that can never be repeated by the factory. The correct fix returns both units to the controlled build standard first.
Repeatable damping starts before production. Incoming shims need thickness inspection, oil needs viscosity and batch tracking, and every torque and charge point needs a numbered tool or gauge. At Yearben, bypass shock builds use serialized torque records, fill volume checks after vacuum bleeding, and nitrogen pressure logs tied to each serial number. Dyno testing is then run on a defined cycle, not a single pull.
A serious supplier establishes a control band for force at multiple velocities and holds every dyno run inside that band. If a shock falls outside the band, it goes back to the bench before it enters the same shipment as the good units.
What Should You Ask a Bypass Shock Supplier About Consistency?
Before placing an order, ask for the dyno protocol and the tolerance. A useful answer names the oil fill method, charge procedure, shim inspection plan, and the force spread the factory accepts at low, mid, and high shaft speed. If the supplier cannot show how it controls those four variables, run-to-run inconsistency will return even after the first correction.
Run-to-run mismatch is rarely a reason to abandon a shock design. In most cases I have worked on, the lower-force unit was built to a different fill, charge, or stack condition than the unit that felt right. Send your current dyno sheets, charge logs, and valve stack settings to info@yearbenshocks.com or call +86-523-86566899. We will compare the two runs against the intended build sheet and confirm which change will bring the shocks into tolerance before you commit to a production batch.
Common Questions About Bypass Shock Inconsistency
Why do two new bypass shocks from the same batch produce different dyno curves?
In most cases, the difference comes from oil fill volume, nitrogen charge, or a shim stack that was assembled one shim off from the drawing. A bypass shock can still look right externally while those internal conditions differ. The fastest check is to run both shocks at the same temperature and compare the low-speed section of the curve first, because that part responds clearly to bleed, charge, and preload changes before the bypass tubes dominate. If the low-speed curves align but high-speed force separates, look at the bypass check valve orientation next.
Is bypass shock inconsistency always a valving problem?
No, and that assumption is one of the most expensive mistakes I see. Valving gets changed when the actual fault is charge pressure, oil fill, or a partially turned bleed screw. Those variables shift the curve at different points, though. If low-speed compression and rebound both move in the same direction, charge or bleed is more likely than a stack error. If the change appears only on rebound, inspect the rebound stack before touching the compression side. That distinction saves a full day of tuning.
How should nitrogen pressure be checked when two runs do not match?
It depends on when the check happens. A shock that is checked before cycling will show a different stabilized pressure than one checked after three full strokes and a short rest. The correct sequence is to charge, cycle the shock through its full stroke, check for pressure drop, then recharge to the target and log the temperature. If both shocks are checked the same way and still differ, the leak path or fill height becomes the next suspect rather than the valving.
How many dyno runs should a supplier perform before shipping a bypass shock?
In production programs I have worked on, the minimum was one warm-up pull followed by three consecutive pulls at the same temperature and charge pressure, with force values plotted against the control band. A single pull is not enough because it can hide a slow-pressure leak or a stack that shifts after the first heat cycle. The supplier should also record which serial number matches which dyno sheet, not just which batch. Share your shock drawing, current shim stack, and mismatched run data, and we will confirm whether the correction is in valving, fill, or charge before you order.
If you’re interested, check out these related articles:
Customized Steering Dampers 24mm
Triple-Bypass-Remote-Reservoir-Shock
Heavy duty seat damper 35mm, Shock Absorber Manufacturer
4X4-Heavy-Duty-Suspension
Customized Lawn Mower damper 24mm