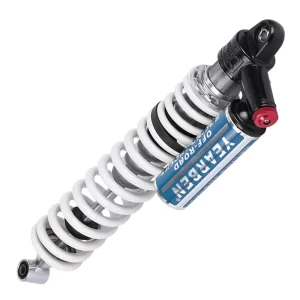
Coilover shock absorber manufacturing converts a set of machined and wound components into an assembly that has to hold consistent damping force across thousands of cycles. Most published explanations stop at naming the piston, shim stack, and coil spring. The real production risk sits earlier, in bore finish, rod chrome thickness, and nitrogen charge verification. As a suspension engineer at TaiZhou Yearben Shock Absorber Technology, I judge a factory by those measured variables before I judge its catalog. This article walks through the production sequence and the quality gates that separate repeatable OEM supply from one-off builds.
Coilover Shock Absorber Component Preparation
The first quality gate starts before assembly. For a coilover damper, the cylinder tube is cut, honed, and checked for roundness. If the bore carries even light scoring, the piston ring and seal will wear quickly once the shock cycles under load. We hone the tube and verify surface finish with a profilometer before any piston enters. The piston rod is ground and chrome plated; rod straightness and chrome adhesion are inspected because a pitted rod destroys the seal head long before the damping curve shows a problem.
| Production step | What we verify | Common defect if skipped |
|---|---|---|
| Cylinder tube honing | Bore roundness and finish | Early seal wear and fading |
| Piston rod chrome plating | Plating thickness and adhesion | Rod pitting and oil leaks |
| Piston machining | Land diameter and groove depth | Inconsistent low-speed damping |
| Spring winding | Free length and rate | Ride height loss after settling |
| Nitrogen charging | Pressure after temperature soak | Aeration and damping fade |
At TaiZhou Yearben, this preparation stage supports more than 200 shock absorber models and an annual production capacity of 1.5 million units. The ability to hold this step is what separates a factory that can ship mixed ATV and UTV programs from a workshop that can only repeat one design.
Piston and Shim Stack Machining Sequence
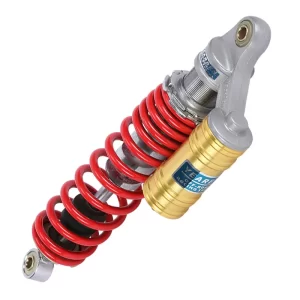
The damping curve is not created by the main body; it is built in the piston and shim stack. We machine piston blanks from steel, then grind the lands and ring grooves to a controlled width and depth. The shim set is assembled in a clean area, because a single reversed shim or a missing preload shim changes the low-speed curve enough to fail a dyno overlay. Production operators work from a build sheet that lists shim diameter, thickness, and order, and the completed stack is photographed before it enters the body.
For adjustable damping shocks, the needle and clicker assembly is calibrated on the same line so that the adjustment range matches the valving target. Oil viscosity is matched to spring rate and vehicle weight; a heavier ATV or UTV usually needs a different piston land profile than a light buggy.
Coil Spring Matching and Preload Setting
Coil springs are wound to a specified free length and rate, then shot peened and powder coated. The spring needs to sit within the damper’s adjustment range, so preload is not set by guesswork. We build a measured spring onto the body, seat the upper and lower perches, and record the installed length. If the spring rate is off, the crossover and ride height change before the shock ever sees a trail.
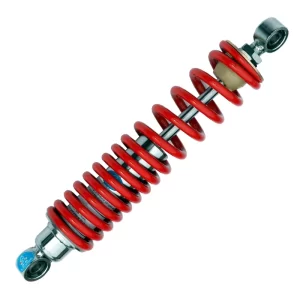
Spring matching matters most on long-travel and multi-rate builds. A dual-rate spring stack has two different windings; each section must be matched to the damper’s shaft travel so the transition happens at the intended ride height. On our off-road coilover lines, the perch position is locked after a dimensional check against the customer’s extended and compressed lengths.
Assembly, Gas Charging, and Leak Verification
Assembly follows a fixed order: piston and shim stack on the rod, seal head prepared, oil filled and bled, then the gas charge. For emulsion coilovers, gas and oil share one body; for piggyback and remote reservoir designs, the separation happens in the reservoir. Yearben offers 0-degree and 90-degree piggyback options plus remote reservoir shocks, and the charge method changes with each configuration. After charging, every unit goes through a leak check and a temperature soak, because a shock that passes cold can still show pressure loss after the gas reaches operating temperature.
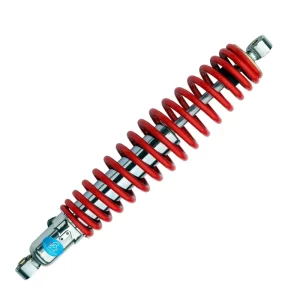
If your program involves long-travel or adjustable damping, confirm charge pressure, reservoir hose length, and dyno matching before freezing the BOM. Send your target spring rate and extended/compressed lengths to info@yearbenshocks.com.
OEM Coilover Pre-Production Checks
Buyers who have been through a failed coilover program usually worry about the same gap: the first article sample looked right, but the production batch did not dyno the same. That happens when pre-production checks stop at dimensions and skip the damping curve overlay, gas pressure decay, and spring rate distribution. Before you commit to an order, narrow the risk by sending the part number, vehicle weight, spring rate, extended and compressed lengths, and expected annual volume. We can confirm bore size, seal specification, and gas pressure for the application, then produce a first article inspection report and production sample for approval.
For custom coilover and multi-SKU programs, the same engineering review applies to custom shocks and struts. Send those target values to info@yearbenshocks.com or call +86-523-86566899 and we will return a feasibility response with a production timeline.
Common Questions About Coilover Shock Absorber Manufacturing
How long does a custom coilover order take from drawing to production samples?
A new custom coilover typically moves from drawing approval to pre-production samples in 30 to 45 days. The range tightens when the design uses an existing bore size, spring rate, and seal configuration. A fully new piston and shim combination adds machining and dyno iteration time, while custom reservoir brackets or hose lengths add coordination with the subassembly supplier. Surface treatments such as anodizing or powder coating also extend the schedule. At Yearben, we lock the production timeline only after the damping curve and extended/compressed lengths are confirmed with the buyer.
Do piggyback and remote reservoir coilovers assemble the same way as emulsion shocks?
A common assumption is that adding a reservoir only increases oil volume, but the assembly difference is where the gas sits. In an emulsion shock, nitrogen and oil share the main body, so the fill and charge sequence happens through one chamber. A piggyback or remote reservoir keeps the gas behind a dividing piston or bladder, which requires a separate vacuum fill and hose assembly step. That extra separation changes how the damper handles heat and shaft displacement, and it adds leak points that must be verified before the unit leaves the line.
Can one factory produce both standard ATV shocks and long-travel coilovers?
It depends on whether the machining and dyno cells are sized for the longer body lengths and the valving range. A factory set up for short ATV shocks may lack the stroke capacity or the reservoir tooling needed for long-travel builds. We run both categories, with standard ATV and UTV shocks alongside long-travel and remote reservoir coilovers. If a buyer wants one supplier for multiple platforms, the audit should confirm the supplier can show dyno data for the longest stroke in the program, not just the base model.
What causes a new coilover to leak from the seal head?
In warranty returns we have analyzed, most early seal head leaks came from rod chrome damage or contamination during assembly rather than a weak seal design. A scratch on the chrome surface cuts the seal lip as the rod cycles, and the leak shows up within the first few hours. Contamination trapped under the seal creates the same result through abrasion. That is why rod handling, clean assembly, and post-assembly pressure decay testing are not optional steps on a production line. If you are seeing early seal leaks on a current batch, send the failure photos and batch number to info@yearbenshocks.com and we will run a root cause review.
If you’re interested, check out these related articles:
Twin-Tube-Hydraulic-Seat-Damper-28MM
Best-Off-Road-Shocks
Remote-Reservoir-Shocks-Manufacturer